When steelmakers and procurement teams search for "graphite electrodes coke," they are usually looking for one specific thing: the carbon feedstock that graphite electrode manufacturers melt, bake, and graphitize into the conductive rods used in electric arc furnaces (EAFs). The term is easy to confuse with the finished electrode itself, but graphite electrode coke is the raw carbon material — most commonly needle coke and selected petroleum coke — that enters production before any electrode is shaped.
This guide explains what graphite electrodes coke actually is, why its quality decides electrode performance, how different coke grades map to regular-power, high-power, and ultra-high-power electrodes, and the parameters buyers should verify before placing an order.
What Is Graphite Electrodes Coke?
Graphite electrodes coke refers to the solid carbonaceous feedstock — principally petroleum-derived coke blended with coal tar pitch binder — used to manufacture graphite electrodes for EAF steelmaking, ladle refining and other high-temperature electric heating processes.
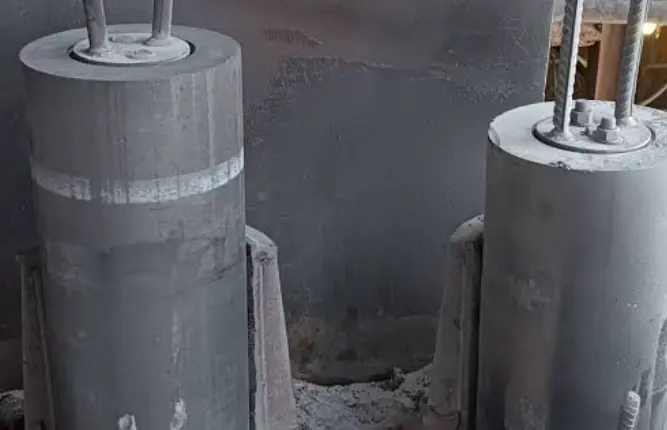
It is not a finished electrode. A finished graphite electrode is a dense, machined cylindrical conductor that carries electric current into the furnace arc. Graphite electrodes coke, by contrast, is the starting black, porous carbon grain that later goes through calcination, forming, baking, pitch impregnation and graphitization before it ever becomes a rod.
In practical trade language, buyers use "graphite electrodes coke" when they mean coke qualified for electrode production: petroleum needle coke for premium grades, and carefully selected sponge or petroleum coke for standard grades. The same word can appear in supplier titles, raw-material inquiries and technical datasheets, which is why separating feedstock from finished product matters in every specification sheet.
Why Coke Is the Decisive Raw Material
A graphite electrode performs three jobs simultaneously inside an EAF: it conducts heavy electric current, survives extreme arc heat, and resists thermal shock as the furnace cycles between charging and melting. Nearly all of these properties originate in the coke grains.
The pitch binder only holds the grains together during forming; the carbon crystal structure that emerges after graphitization comes from the coke. If the coke has high ash, high sulfur or a high coefficient of thermal expansion (CTE), the final electrode will show higher resistivity, faster consumption, poorer thermal-shock resistance and a higher risk of vertical cracking — even if every downstream process step is executed correctly. That is why experienced buyers treat graphite electrode coke quality as a purchasing decision rather than a secondary detail.
Needle Coke vs. Sponge and Petroleum Coke
Electrode production draws on two main coke families, each matched to an electrode power class.
Needle Coke
Needle coke is a premium crystalline carbon produced by delayed coking of specific heavy aromatic petroleum feedstocks. It shows a visible needle-like fiber structure, high graphitizability, a low coefficient of thermal expansion and good electrical conductivity. These characteristics make needle coke the standard feedstock for ultra-high-power (UHP) graphite electrodes, where the electrode carries the heaviest current loads and endures the most aggressive arc conditions. Industry references consistently describe needle coke as essential for UHP production because no equally performing substitute exists at that power level.
Sponge Coke and Selected Petroleum Coke
Sponge coke has high chemical reactivity, low impurity content and a spongy porous texture. When screened for consistent ash, sulfur and grain size, it feeds regular-power (RP) and many high-power (HP) electrode grades. General-grade petroleum coke that fails these impurity limits is typically diverted to anodes, carbon additives or fuel markets rather than electrode production.
Key Quality Parameters for Graphite Electrodes Coke
When evaluating graphite electrodes coke, professional specifications should state the following parameters rather than vague claims such as "high quality":
|
Parameter
|
Why it matters
|
|
Ash content
|
Mineral impurities raise resistivity and weaken the graphitized body; lower is generally better for electrodes.
|
|
Sulfur content
|
Excess sulfur contributes to gas evolution, porosity and surface blowholes after baking.
|
|
Coefficient of thermal expansion (CTE)
|
Low CTE means the graphitized electrode resists thermal shock; needle coke is valued here above all.
|
|
Electrical resistivity
|
Influences how much current the finished electrode conducts efficiently.
|
|
Volatile matter
|
Must be driven off by calcination before forming; stable values reduce baking defects.
|
|
True density and grain size
|
Affect green forming, density uniformity and machining of the final rod.
|
Buyers should request a mill test report covering these figures for each batch rather than relying on a general product description.
From Coke to Finished Electrode: The Production Chain
Understanding the route helps explain why feedstock selection happens first:
- Calcination — Raw coke is heat-treated to remove moisture and volatiles and stabilize its structure.
- Crushing and grading — Coke is milled into controlled grain sizes and sized fractions.
- Mixing — Coke grains are blended with coal tar pitch, which acts as the binder.
- Forming — The paste is extruded or molded into a "green" electrode cylinder.
- Baking — The green body is baked at elevated temperature to carbonize the pitch.
- Impregnation — Premium grades are impregnated with additional pitch under pressure and re-baked to fill pores and raise density.
- Graphitization — The baked body is heated to roughly 2,800–3,000 °C in an Acheson or lengthwise graphitization furnace, where disordered carbon reorganizes into the ordered hexagonal graphite lattice, sharply lowering resistivity.
- Machining — The graphitized rod is cut, threaded and fitted with nipples for installation.
How Coke Grade Maps to RP, HP and UHP Electrodes
|
Electrode class
|
Typical furnace use
|
Typical coke basis
|
|
RP (Regular Power)
|
Lower-current melting and smaller furnaces
|
Selected sponge / petroleum coke
|
|
HP (High Power)
|
Medium-current operation
|
Blended selected coke, higher-density baking
|
|
UHP (Ultra-High Power)
|
Large modern EAFs, high-current scrap melting
|
Needle coke with low CTE and controlled impurities
|
Matching the coke basis to the intended power class avoids the common mismatch of over-specifying feedstock for a small furnace or under-specifying it for a high-current line.
Common Questions About Graphite Electrodes Coke
Is graphite electrodes coke the same as a graphite electrode?
No. Graphite electrodes coke is the raw carbon feedstock; the graphite electrode is the finished, machined conductive rod after baking and graphitization.
Which coke is used for UHP electrodes?
Needle coke, because its low coefficient of thermal expansion and high graphitizability support the current density and thermal shock of ultra-high-power EAF operation.
What quality figures should a buyer request?
Ash, sulfur, CTE, electrical resistivity, volatile matter, true density and grain size, provided on a batch mill test report.
Can any petroleum coke be used for electrodes?
No. Only coke screened for low impurities, stable volatiles and suitable structure qualifies for electrode grades; ordinary fuel-grade petroleum coke is not suitable.
Conclusion
Graphite electrodes coke is the carbon foundation of every electrode that melts scrap in an EAF. Needle coke anchors the UHP segment, selected sponge and petroleum coke serve RP and HP production, and the batch-level parameters — ash, sulfur, CTE, resistivity, volatile matter and density — determine whether the finished electrode lasts or consumes prematurely. For steelmakers, foundries and electrode buyers, specifying the right graphite electrodes coke on the front end prevents most performance problems on the shop floor.
To discuss qualified coke-based electrode supply, grade matching and technical specifications, contact the ZGTD team here: Contact Us — https://www.zgtdts.com/contact-us/
Post time: 10-22-2026